Over 10,000+ customers' choice, Focus on screening industry 40+ years
Catalyst powder typically needs to be transferred to mixers, screening machines, reactors, or other processing equipment. Although manual feeding is straightforward, it can create several challenges in daily production.
Dust can become airborne during bag emptying. When powder is poured from bags or containers into processing equipment, the falling material can disturb surrounding air and cause fine particles to spread beyond the feeding area.
Repeated handling increases material exposure. If materials must be manually transferred, temporarily stored, and fed multiple times, they have more opportunities to come into contact with the surrounding environment.
Manual operations can affect feeding schedules. Operators need to handle material movement, bag opening, pouring, and cleaning. Feeding rates may therefore depend on staffing levels and work arrangements.
More dust can increase cleaning and housekeeping demands. Powder settling on equipment surfaces, floors, and nearby facilities may require more frequent cleaning and add to routine production management tasks.
For catalyst production lines that require continuous feeding or material delivery to multiple workstations, improving the feeding method can help streamline material handling.
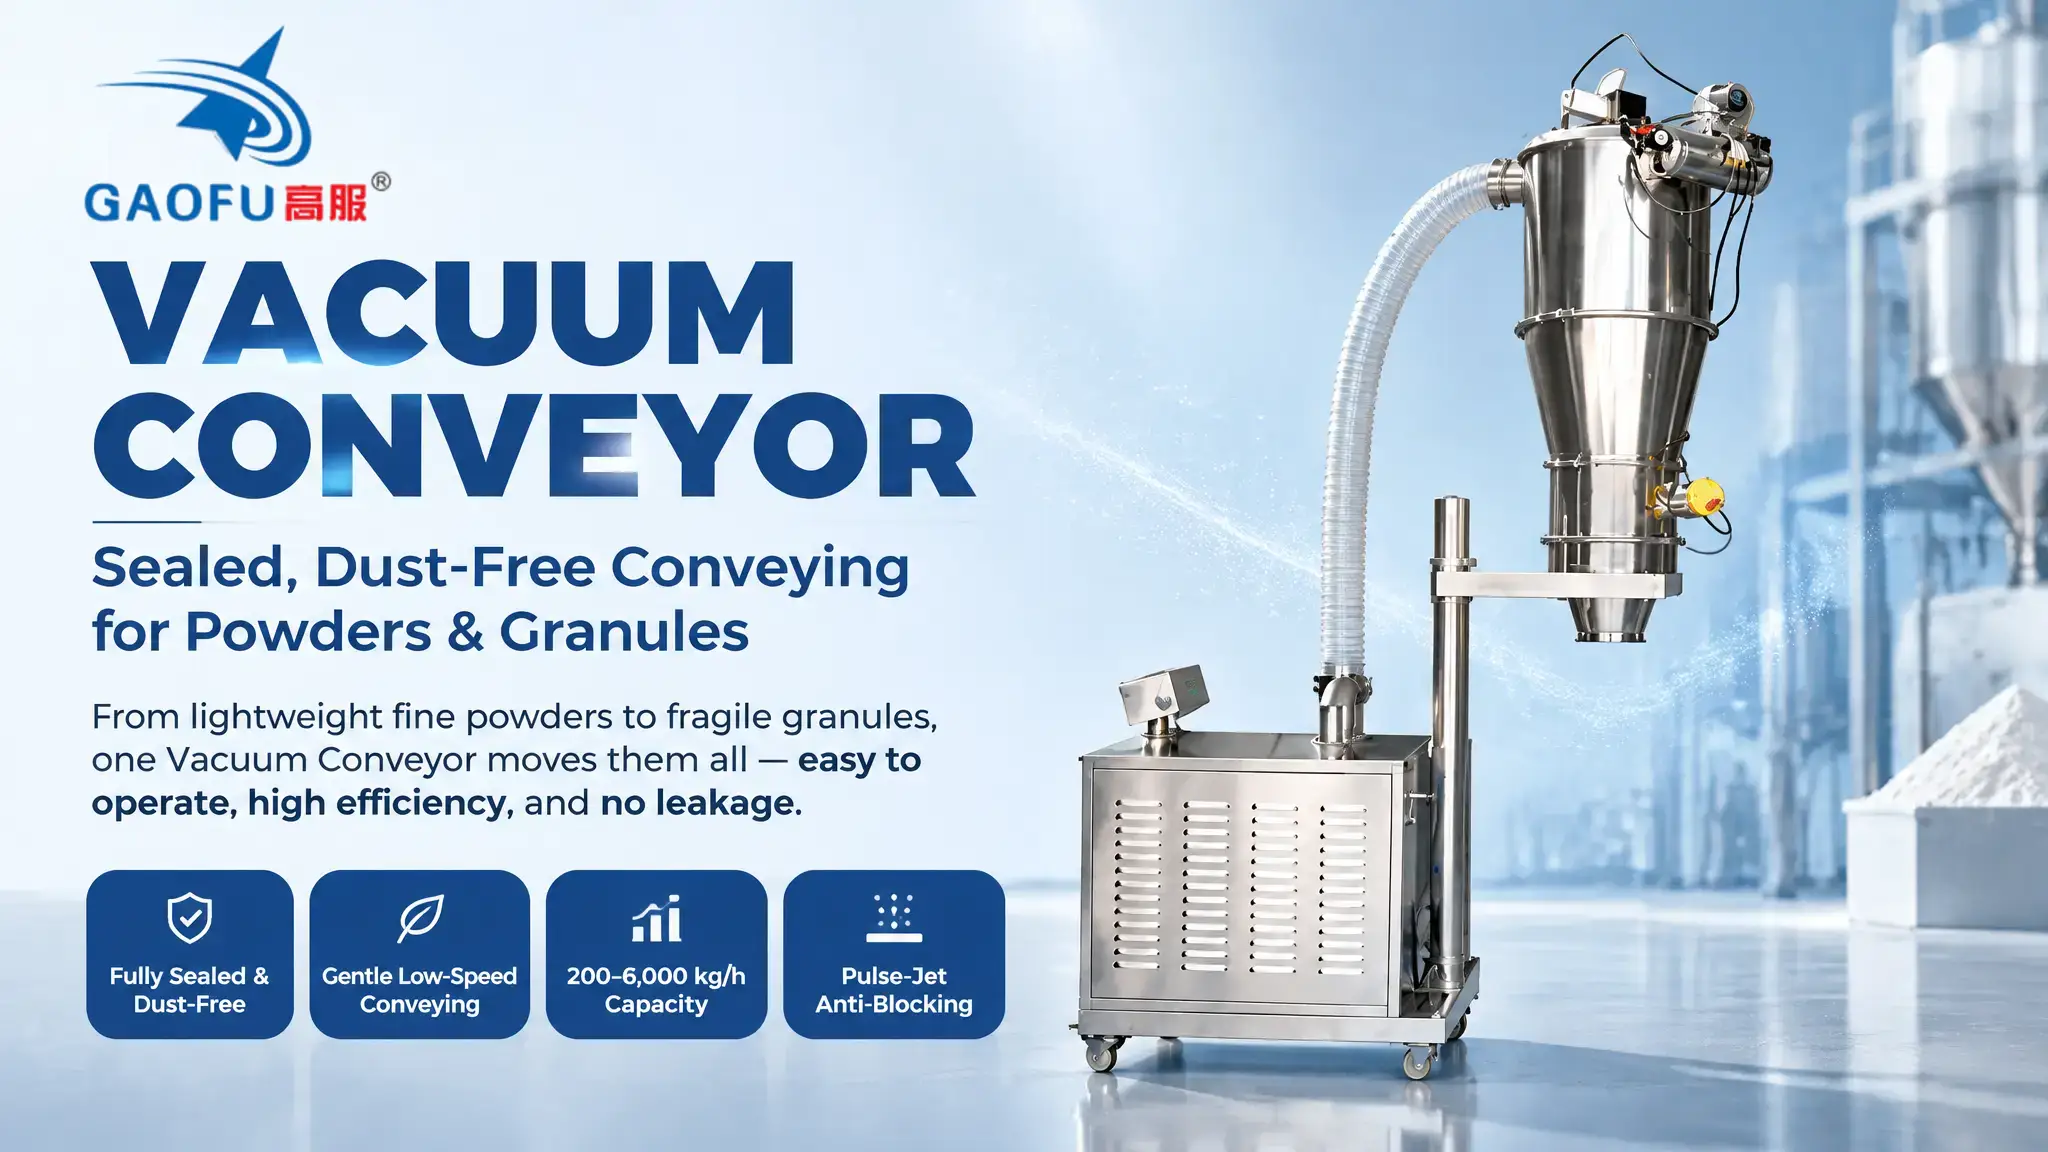
Gaofu Machinery's Vacuum Conveyor operates on the principle of negative-pressure conveying. During operation, the vacuum power unit creates a pressure difference within the system. Airflow draws material from the feeding point into the conveying pipeline and transports it to the designated receiving unit.
The basic operating process can be summarized as follows:
Material feeding → Vacuum suction → Pipeline conveying → Filtration and separation → Material discharge
When the material reaches the receiving unit, the separation structure separates the powder from the conveying air. The material is discharged into the downstream equipment, while the filtered air is handled according to the system design.
Compared with manual handling and open pouring, this arrangement integrates several transfer steps into a relatively enclosed process. It helps reduce the need for operators to handle powder directly or repeatedly feed material by hand.
The specific equipment structure, filtration method, and discharge arrangement should be selected according to the actual model and process requirements. Not every configuration includes the same standard features.
The Vacuum Conveyor connects the feeding point and receiving equipment through pipelines, reducing the need for material to be exposed to the open environment during transfer.
For dust-prone catalyst powders, this arrangement can help reduce the risk of dust escaping during feeding and improve housekeeping conditions in the production area.
The system can also be configured with suitable filtration equipment to help prevent powder from being carried downstream with the conveying airflow. Actual dust control performance depends on pipeline sealing, filter specifications, maintenance, and the plant's overall dust collection system.
Traditional feeding often requires operators to repeatedly lift, carry, and pour materials. A Vacuum Conveyor can perform material suction and transfer according to the process requirements, reducing the number of manual handling steps.
Manufacturers can integrate the system with storage equipment, mixers, screening machines, and other processing units according to their production schedules. This helps coordinate material flow between different stages while reducing repetitive operator tasks.
In chemical plants where equipment is distributed across different areas, manual material transfer may involve several intermediate steps. A Vacuum Conveyor allows pipelines to be arranged according to the facility layout, connecting the feeding point directly to the target equipment where appropriate.
This pipeline-based approach can help reduce intermediate handling and temporary storage. It also allows manufacturers to plan material transfer routes around their production line layout.
The actual conveying distance, vertical lift, and number of pipeline bends must be evaluated according to material characteristics and system capacity.
When handling different catalyst types or production batches, manufacturers need to consider material residue and potential cross-batch carryover. Relatively enclosed conveying can reduce direct contact between powder and the surrounding environment, supporting material cleanliness management.
For multi-product production lines, cleaning and changeover procedures should be established based on pipeline design, equipment disassembly requirements, and material characteristics. Proper cleaning and inspection can help manage residual material, although enclosed conveying alone cannot guarantee the complete elimination of cross-contamination.
A Vacuum Conveyor can be connected to different types of production equipment according to the manufacturing process. Typical applications include:
Feeding mixers: Transfer catalyst raw materials into mixing equipment while reducing manual feeding operations.
Supplying screening machines: Connect powder conveying with particle size classification using a vibratory screen or other screening equipment.
Feeding metering systems: Deliver materials to weighing or metering equipment for subsequent batching operations.
Supplying packaging machines or storage hoppers: Improve material flow between production and packaging stages.
With an appropriate combination of feeding units, pipelines, and receiving equipment, manufacturers can develop a material transfer arrangement that matches their production requirements.
Catalyst materials vary considerably in their physical and chemical properties. Selecting a Vacuum Conveyor based only on conveying distance or equipment appearance may result in a system that does not fully match the application. Gaofu Machinery recommends evaluating the following factors before selecting equipment:
Particle size and flowability: Fine powders, granules, and materials prone to agglomeration may require different feeding methods and conveying parameters.
Bulk density and conveying capacity: Bulk density, required conveying volume, and production schedules should be considered when determining system specifications.
Particle strength: For fragile catalyst granules, evaluate airflow velocity, pipeline bends, and discharge methods to help manage abrasion and the generation of additional fines.
Chemical properties: For corrosive, toxic, or otherwise sensitive catalysts, review the material safety data sheet (SDS) to determine suitable contact materials, sealing arrangements, and filtration requirements.
Dust-related safety risks: If the material may generate combustible dust, a professional hazard assessment is necessary. Appropriate protective measures must be designed according to applicable requirements. A standard Vacuum Conveyor should not be assumed to provide explosion protection.
Installation conditions: The feeding location, receiving equipment height, pipeline routing, and maintenance access all influence the final system design.
For catalysts sensitive to humidity, oxygen, or temperature, manufacturers should also evaluate whether dedicated gas protection or environmental control measures are required. Such features must be designed separately according to material properties and safety requirements; they should not be regarded as standard functions of every Vacuum Conveyor.
Moving from manual handling to negative-pressure pipeline conveying changes more than the way materials enter processing equipment. It can also improve how feeding operations and personnel tasks are organized across the production line.
Gaofu Machinery's Vacuum Conveyor is designed for powder conveying applications in the chemical industry. The system can be configured according to catalyst characteristics, conveying distance, required capacity, and facility layout.
Through relatively enclosed pipeline conveying, automatic vacuum feeding, and integration with downstream equipment, the system helps reduce open feeding operations, lower the risk of dust dispersion, and improve material flow between production stages.
It is important to note that a Vacuum Conveyor primarily performs material transfer. It cannot independently guarantee the original catalytic activity, chemical purity, or final product quality of a catalyst. These properties must be managed through appropriate manufacturing processes, storage conditions, environmental controls, and quality testing.
For chemical manufacturers looking to optimize manual feeding operations and improve powder handling conditions, Gaofu Machinery can provide Vacuum Conveyor configuration recommendations based on actual material characteristics and production requirements. The goal is to support more organized catalyst powder transfer and further automation of the production line.
Chemical Industry Client Testimonials
Wanhua Chemical, Yuntianhua Group, Kingfa Science & Technology, Formosa Plastics Group, China Pingmei Shenma Group, Kemai Co., Ltd., Luxi Chemical, Liby Group, Oriental Yuhong, Davco, Chenming Group, Guanhao High-Tech
Kaifei Chemical, Sunsine Chemical, Weilin Co., Ltd., Xuyang Group, 3Trees, Maydos, Loyal Group (Kingpor Group), AkzoNobel, CSSC Hanguang, Haike Group, Nice Group, Taishan Fiberglass, Wanhua, Red Eagle, China XLX Fertiliser (Xinlianxin), CCtech Catalysis, China National Bluestar, Sakura Paint, ITANOS, Yanggu Huatai, Sennics, Longxing Chemical Group, Tunhe Co., Ltd., GHW International, Jianye Chemical, Finehope
Fortune 500 Client Testimonials
CNPC、CSCEC、Sinochem Holdings、CRCC、China Minmetals Corporation、CNOOC、CR、Sinopharm、CHN Energy、COFCO Corporation、Huawei Technologies、PowerChina、CITIC Group、Wuchan Zhongda Group、NORINCO、Chalco、CNBM、 Shaanxi Coal and Chemical Industry Group、Ansteel Group、CETC、CSSC、CASC、CEC、Jinchuan Group、CASIC、Conch Cement、CNNC、SPH、Shanxi Coking Coal Group、 Zhongtai Chemical、GPHL、DEC、Sinosteel Corporation、MCC、China National Salt Industry Chemical、China Baowu Steel Group、China Animal Husbandry Industry Co., Ltd.、CECEP
About Gaofu
Xinxiang Gaofu Machinery Co., Ltd. was founded back in the 1980s. With over 40 years of development, it has been certified as a National-level Specialized, Refined, Unique & Innovative Little Giant Enterprise, National Green Factory, National High-tech Enterprise, and National Intellectual Property Advantage Enterprise, and serves as the President Unit of China Vibration Screening Industry Association.
The company is accredited with the Henan Provincial Industrial Design Center, Henan Provincial Engineering Technology Research Center for Intelligent On-line Screening System, and Xinxiang Municipal Engineering Technology Research Center for Fine Screening.
Gaofu has obtained more than 500 patents including invention patents, utility model patents and design patents, been awarded the Science and Technology Achievement Prize issued by the Ministry of Industry and Information Technology of China, and participated in drafting and formulating 4 national standards.
Gaofu's product portfolio covers multiple series and hundreds of specifications, including vibrating screening equipment, conveying equipment, coal crushing equipment, filtration equipment and automatic material handling systems.
Core products include vibrating screens, screening machines, vibratory sifters, rotary vibrating screens, ultrasonic vibrating screens, linear vibrating screens, airflow screens, gyratory screens, roller screens, dewatering screens, bar screens, vacuum feeding machines, dust-free feeding stations, bulk bag feeding stations, feeding systems, automatic powder feeding systems, automatic slag-discharging filters, leaf filters, clay filters, toothed roll crushers, coal crushers and other machinery.
These products are widely applied in food, pharmaceutical, chemical, metallurgy, construction materials, mining, thermal power, environmental protection and many other industries, winning recognition and trust from over 10,000 clients worldwide.
Gaofu products enjoy strong sales across Greater China, and are exported to more than 100 countries and regions such as Russia, Canada, the United States, New Zealand, Japan, Brazil and South Africa.
Upholding the corporate mission of Improving material quality & efficiency to fully satisfy customer demands, Gaofu maintains long-term partnerships with clients to achieve win-win development.
At present, Gaofu is an official qualified supplier for numerous Fortune Global 500 enterprises, including CNPC, Sinopec, Sinochem Holdings, China Resources Group, Sinopharm Group, COFCO, China National Building Material, China Aerospace Science and Technology Corporation, Jinchuan Group and more.
Gaofu Machinery ranks No.1 in global sales volume of vibrating screens.
In May 2024, Frost & Sullivan, a world-renowned international consulting firm, issued a Market Position Verification Certificate confirming that Gaofu achieved the world's largest shipment volume of vibrating screens in the global market in 2023.