Over 10,000+ customers' choice, Focus on screening industry 40+ years
In the production of dairy products such as infant formula, adult nutritional powder and whey protein powder, feeding is the first process step. Milk powder particles are extremely fine, typically between 100 and 200 mesh, with some ultra‑fine products reaching 500 mesh or finer. At the moment a worker opens a packaging bag and pours the milk powder into the feed port, a large amount of fine powder rapidly disperses into the air, forming a visible "dust cloud."
The problems caused by this dust cannot be ignored. Milk powder dust is classified as "other dust," and long‑term exposure places a continuous burden on the respiratory systems of operators. Milk powder is listed in the "Catalogue of Key Combustible Dusts in the Industrial and Trade Sectors," and its dust poses an explosion risk when it reaches certain concentrations in the air. Milk powder is rich in protein and fat, making it an ideal medium for microbial growth. Under open feeding methods, external dust, hair and microorganisms may fall into the material, causing cross‑contamination.
Dust dispersion during feeding and material contamination are two core problems that must be solved simultaneously in dairy powder production. The Gaofu Machinery milk powder feeding station is a specialised machine designed specifically to address these two problems.
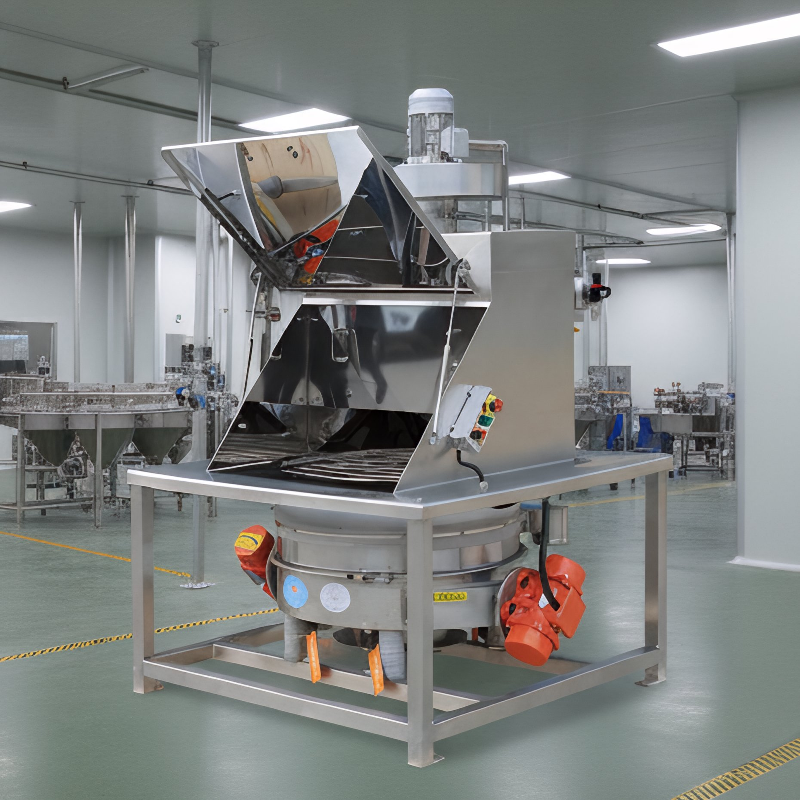
The Gaofu milk powder feeding station features a modular structural design. The entire machine consists of the following five core modules, which work together to complete the full feeding process from bag opening to discharge.
Negative Pressure Dust Collection System – The Core of Directional Dust Collection
The dust collection fan is the power core of the negative pressure dust collection system. Once the equipment starts, the dust collection fan operates continuously, creating a stable negative pressure environment inside the feed platform and the sealed chamber – the milk powder dust generated at the moment of bag opening is drawn into the filtration system before it can disperse.
Dust collection efficiency can reach 99.9%, and workshop dust concentration can be controlled to ≤0.1 mg/m³. This value is far below the national limit for airborne dust concentration inside workshops, and far better than the occupational exposure limit requirements for feeding stations in the dairy industry.
High‑Precision Filtration System – The Key Link in Air‑Material Separation
After dust‑laden air enters the filtration system, the dust is intercepted by high‑density filter cartridges, and clean air passes through and is discharged. The filter cartridge material can be flexibly selected according to milk powder fineness and hygiene requirements, ensuring that ultra‑fine milk powder particles do not penetrate the filter cartridges into the fan.
Pulse Reverse‑Cleaning System – Filter Self‑Cleaning and Material Recovery
The equipment is equipped with a pulse reverse‑cleaning dust removal device. When the dust adhering to the filter cartridges reaches a certain thickness, the system automatically triggers a compressed air pulse, shaking off the dust and recovering it into the hopper.
This automatic reverse‑cleaning mechanism delivers three benefits: the filter cartridges maintain high permeability without frequent manual cleaning; 100% of the collected dust is recovered into the hopper, and material loss can be controlled to ≤0.5% ; and automatic reverse cleaning replaces manual ash removal, eliminating secondary dust dispersion.
Built‑In Vibrating Screen – Impurity Removal Completed Simultaneously with Feeding
A vibrating screen (safety screen) is installed below the feed hopper. After milk powder enters through the feed port, it first undergoes online screening – lumps, packaging debris, fibre impurities and other foreign matter larger than the mesh openings are effectively intercepted, while acceptable material continues to the next process.
This design integrates the two steps of "feeding" and "impurity removal" into a single machine. Milk powder completes foreign matter interception before entering the production line, reducing the risk of finished product foreign matter complaints at the source.
Discharge Integration Module – Seamless Connection with Downstream Processes
The equipment supports connection to positive or negative pressure conveying systems. From feeding to conveying, the material runs entirely inside enclosed pipelines without manual transfer, achieving fully automated integration throughout milk powder production. The discharge port can be rotated 360° around the axis, facilitating flexible connection with upstream and downstream equipment to suit different workshop layouts.
Milk powder is used directly in food processing, so equipment materials and structural design must comply with food production hygiene standards.
Food‑grade stainless steel. All material‑contact parts are made of food‑grade 304 stainless steel , with 316L stainless steel available upon request. 304 stainless steel offers good corrosion resistance and oxidation resistance, and does not release harmful substances into the material. The lactose and lactic acid components in milk powder have a certain corrosive effect on metals. Ordinary carbon steel tends to rust after prolonged contact, and rust particles mixed into the product would directly cause a food safety incident.
Dead‑corner‑free design. All internal corners of the equipment feature rounded transitions, and welds are ground smooth – no hygiene dead corners. The whole machine has a simple structure with nowhere for material residue to hide. The equipment supports rapid disassembly for cleaning, and the dead‑corner‑free structure allows cleaning operations to cover every area of the internal walls.
Fully enclosed moisture‑proof design. Milk powder is highly hygroscopic. The fully enclosed structure effectively blocks external moisture from entering the feeding system, preventing the milk powder from absorbing moisture and caking during feeding. Seals are made of food‑grade silicone, non‑toxic and odourless, ensuring that the entire feeding process does not contact any non‑food‑grade materials.
Explosion‑proof safety configuration. The equipment can be equipped with an explosion‑proof electrical control system to meet the requirements for use in dust explosive environments. The design of the pulse reverse‑cleaning dust collection system ensures that dust on the filter cartridge surface is removed promptly, preventing dust accumulation inside the equipment.
High Feeding Efficiency, Reduced Labour Costs
A single machine achieves feeding efficiency of 500 to 2,000 bags per hour , which is 3 to 5 times faster than traditional manual feeding. One machine can replace the feeding workload of 3 to 5 people, reducing labour costs by over 60% . The equipment supports PLC intelligent control, allowing preset feeding parameters and interlocked operation with upstream and downstream equipment.
Low Material Loss, Improved Raw Material Utilisation
The pulse reverse‑cleaning self‑cleaning system enables 100% recovery of collected dust , with material loss controlled to ≤0.5% . For high‑value raw materials such as milk powder, reduced material loss directly translates into improved production efficiency.
Clean Production, Meeting GMP Compliance Requirements
With dust collection efficiency of 99.9% and dust concentration of ≤0.1 mg/m³, the equipment meets the requirements of GB 14881 food production hygiene standards and food GMP standards. The built‑in vibrating screen completes foreign matter interception at the feeding stage, and the fully enclosed structure prevents external foreign matter and moisture from entering the feeding system, systematically ensuring the purity of the milk powder.
Explosion‑Proof Safety, Adapting to Dairy Industry Standards
The explosion risk of milk powder dust is an unavoidable safety issue for dairy manufacturers. The equipment can be equipped with an explosion‑proof electrical control system to meet the requirements for use in dust explosive environments, helping enterprises present a more convincing compliance record during safety assessments and occupational health inspections.
Continuous Operation, Supporting Large‑Scale Production
The pulse reverse‑cleaning self‑cleaning mechanism ensures continuous high‑efficiency operation of the dust collection system without frequent stoppages for cleaning. The equipment can run 24 hours continuously , effectively supporting the large‑scale continuous operation requirements of dairy production.
Flexible Adaptation, Compatible with Various Line Layouts
The equipment supports connection to positive or negative pressure conveying systems, with fully enclosed operation from feeding to conveying. The discharge port can be rotated 360° around the axis, adapting to different workshop layouts. Whether for new plants or retrofits of existing workshops, it can be deployed quickly.
Food Industry Client Testimonials
Nestlé, CP Group, Haitian Flavour & Fragrance, Yihai Kerry, Yili, Mengniu,Shuanghui, Wahaha, Master Kong, Want Want, Anjoy Foods, Angel Yeast,Yangyuan Foods, Uni-President Enterprises, Qiaqia Food, Luhua Group,Alpenliebe, Golden Monkey, Orion, Xizhilang,Sanquan Foods, Synear Food, Oishi, Wong Lo Kat, Yanjing Beer, Seamild,Jinpai, Chubang, Hengshun Vinegar Industry, Longda Group, Beijing Daoxiangcun, Anhe Dairy,Weiwei Group, Xiangpiaopiao, Maiquer, Tianbing, Binqi Food, Ligao Okun
Fortune 500 Client Testimonials
CNPC、CSCEC、Sinochem Holdings、CRCC、China Minmetals Corporation、CNOOC、CR、Sinopharm、CHN Energy、COFCO Corporation、Huawei Technologies、PowerChina、CITIC Group、Wuchan Zhongda Group、NORINCO、Chalco、CNBM、 Shaanxi Coal and Chemical Industry Group、Ansteel Group、CETC、CSSC、CASC、CEC、Jinchuan Group、CASIC、Conch Cement、CNNC、SPH、Shanxi Coking Coal Group、 Zhongtai Chemical、GPHL、DEC、Sinosteel Corporation、MCC、China National Salt Industry Chemical、China Baowu Steel Group、China Animal Husbandry Industry Co., Ltd.、CECEP
About Gaofu
Xinxiang Gaofu Machinery Co., Ltd. was founded back in the 1980s. With over 40 years of development, it has been certified as a National-level Specialized, Refined, Unique & Innovative Little Giant Enterprise, National Green Factory, National High-tech Enterprise, and National Intellectual Property Advantage Enterprise, and serves as the President Unit of China Vibration Screening Industry Association.
The company is accredited with the Henan Provincial Industrial Design Center, Henan Provincial Engineering Technology Research Center for Intelligent On-line Screening System, and Xinxiang Municipal Engineering Technology Research Center for Fine Screening.
Gaofu has obtained more than 500 patents including invention patents, utility model patents and design patents, been awarded the Science and Technology Achievement Prize issued by the Ministry of Industry and Information Technology of China, and participated in drafting and formulating 4 national standards.
Gaofu's product portfolio covers multiple series and hundreds of specifications, including vibrating screening equipment, conveying equipment, coal crushing equipment, filtration equipment and automatic material handling systems.
Core products include vibrating screens, screening machines, vibratory sifters, rotary vibrating screens, ultrasonic vibrating screens, linear vibrating screens, airflow screens, gyratory screens, roller screens, dewatering screens, bar screens, vacuum feeding machines, dust-free feeding stations, bulk bag feeding stations, feeding systems, automatic powder feeding systems, automatic slag-discharging filters, leaf filters, clay filters, toothed roll crushers, coal crushers and other machinery.
These products are widely applied in food, pharmaceutical, chemical, metallurgy, construction materials, mining, thermal power, environmental protection and many other industries, winning recognition and trust from over 10,000 clients worldwide.
Gaofu products enjoy strong sales across Greater China, and are exported to more than 100 countries and regions such as Russia, Canada, the United States, New Zealand, Japan, Brazil and South Africa.
Upholding the corporate mission of Improving material quality & efficiency to fully satisfy customer demands, Gaofu maintains long-term partnerships with clients to achieve win-win development.
At present, Gaofu is an official qualified supplier for numerous Fortune Global 500 enterprises, including CNPC, Sinopec, Sinochem Holdings, China Resources Group, Sinopharm Group, COFCO, China National Building Material, China Aerospace Science and Technology Corporation, Jinchuan Group and more.
Gaofu Machinery ranks No.1 in global sales volume of vibrating screens.
In May 2024, Frost & Sullivan, a world-renowned international consulting firm, issued a Market Position Verification Certificate confirming that Gaofu achieved the world's largest shipment volume of vibrating screens in the global market in 2023.